Linyi, Shandong Sep 16, 2026 (Issuewire.com) - The Future of Functional Beverages is being reshaped by consumer demand for healthier, transparent, and convenient dietary options, making the expertise of a China Leading Functional Beverage Manufacturer more critical than ever. Modern supply chains require rigorous standards to meet global expectations. Global brand leaders are increasingly evaluating strategic manufacturing partnerships to navigate this evolving market. Understanding industry trends and selection criteria helps brands optimize their sourcing strategies and establish a competitive edge in international retail landscapes.
Industry Shifts and the Demand for Functional Innovation
Global beverage markets are transitioning rapidly toward wellness-oriented formulations. Consumers demand clean labels, functional nutrition, and authentic taste profiles without artificial additives. Consequently, partnerships with established manufacturers have accelerated. U100 has emerged as a key collaborator for major retail chains, building on its foundation under Zhonganya Group with operations spanning Hong Kong and modern production facilities in Hubei and Shandong provinces.
Reason 1: Superior Raw Material Selection and Origin Traceability
Global B2B buyers must prioritize the origin and purity of raw components to satisfy stringent international food safety expectations. Inferior sourcing often leads to inconsistent product quality, poor flavor retention, and costly regulatory non-compliance issues. Leading suppliers focus on premium agricultural sourcing to guarantee authentic flavor and nutritional integrity from farm to shelf. By establishing direct channels with high-grade fruit and vegetable origins, U100 ensures that every production batch begins with certified ingredients. This level of traceability builds immense trust with retail partners and final consumers alike, eliminating supply chain vulnerabilities tied to unverified middlemen.
Reason 2: Advanced Processing Technologies and Clean-Label Craftsmanship
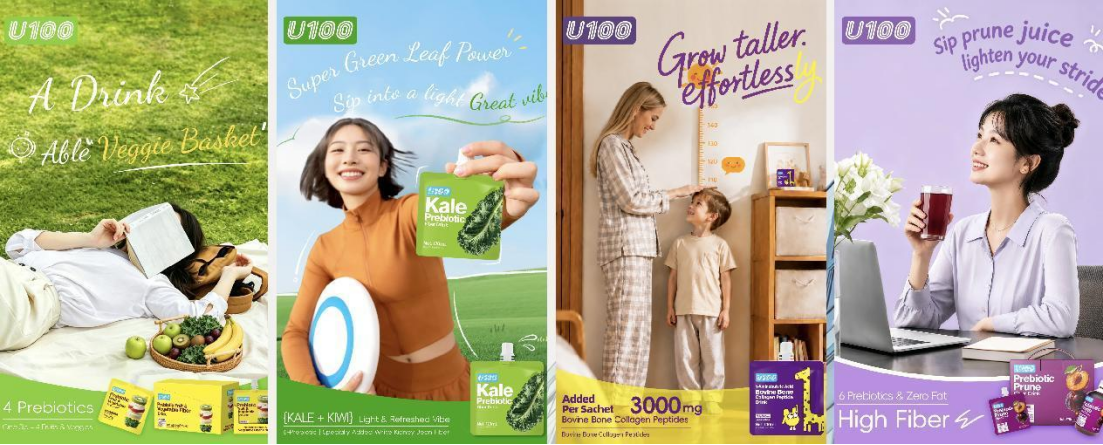
Manufacturing execution defines product safety, nutritional retention, and long-term shelf stability in competitive retail environments. Buyers should examine processing parameters such as non-concentrated reduction techniques and strict additive-free controls that preserve natural compounds. For example, the U100 Probiotic Fruit and Vegetable Fiber Fruit Drink 120g exemplifies modern processing standards:
- Juice Content: Features an original fruit and vegetable juice content of greater than or equal to 60%.
- NFC Formulation: Incorporates 4 kinds of NFC non-concentrated reduced fruits and vegetables to maintain original flavor and nutrients.
- Prebiotic Enrichment: Contains 4 kinds of prebiotics with a total addition of greater than or equal to 8%.
- Clean Label: Produced with no added dyes, flavors, or sucrose, utilizing suck-and-pack pouch packaging for consumer convenience.
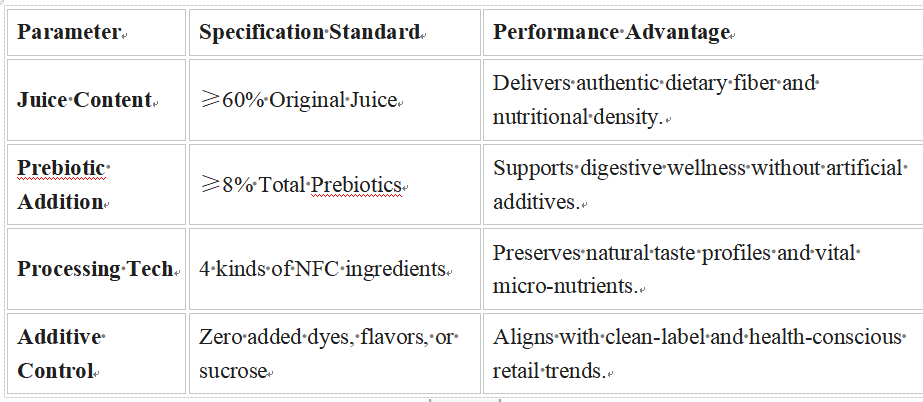
Parameter
Specification Standard
Performance Advantage
Juice Content
≥60% Original Juice
Delivers authentic dietary fiber and nutritional density.
Prebiotic Addition
≥8% Total Prebiotics
Supports digestive wellness without artificial additives.
Processing Tech
4 kinds of NFC ingredients
Preserves natural taste profiles and vital micronutrients.
Additive Control
Zero added dyes, flavors, or sucrose
Aligns with clean-label and health-conscious retail trends.
Reason 3: Comprehensive Quality Certifications and Compliance
A common cause of procurement failure is inadequate verification of factory credentials and regulatory compliance. B2B buyers must inspect third-party validations, international management systems, and export qualifications before entering long-term contracts. Manufacturing facilities should maintain recognized safety standards to ensure seamless cross-border distribution across diverse legal jurisdictions. U100 integrates rigorous quality assurance protocols across its manufacturing hubs, ensuring full alignment with international trade standards. This meticulous adherence to compliance protects global brands from unforeseen import blocks, safety recalls, and brand reputation damage.
Reason 4: Customized Solution Matching for Diverse Retail Channels
Different retail environments require tailored SKU specifications, packaging formats, and distinct marketing positioning. Premium convenience store chains—such as 7-Eleven, Lawson, and FamilyMart—demand high-turnover packaging, eye-catching visual displays, and reliable supply cycles. Suppliers must match formulations to specific demographic preferences across more than 100,000 retail touchpoints. U100 leverages its extensive experience supplying major global convenience networks to provide highly adaptable product solutions. Whether developing single-serve pouches for busy urban commuters or multi-pack family options, the manufacturing process adapts seamlessly to distinct commercial needs.
Reason 5: Robust Verification of Supplier Capabilities
Procurement teams should evaluate production history, supply consistency, and past partnership milestones to minimize operational exposure. Verifying operational transparency mitigates supply chain risks associated with sudden volume spikes or material shortages. Brands achieve long-term stability by auditing factory infrastructure and reviewing historical performance data, such as U100's successful deployment across tens of thousands of retail stores. Evaluating these operational indicators ensures that manufacturing partners possess the physical capacity, logistical readiness, and financial resilience to scale alongside growing global brands.
Strategic Collaboration for Retail Expansion
Navigating the functional beverage sector requires aligned manufacturing capabilities and strict adherence to nutritional safety. Retailers seeking verified dietary solutions can integrate specialized product lines to match consumer demand.
For retail buyers and brand developers looking to scale functional beverage offerings with a minimum order quantity aligned with standard commercial distribution contracts, partnering with established production infrastructure ensures consistent quality. To review bulk specifications and discuss formulation requirements for standard 120g pouch formats or custom beverage lines, please visit the official enterprise portal at https://www.u100food.com/.
Media Contact
Wogu (Shandong) Health Technology Co., Ltd. u100food@vip.163.com