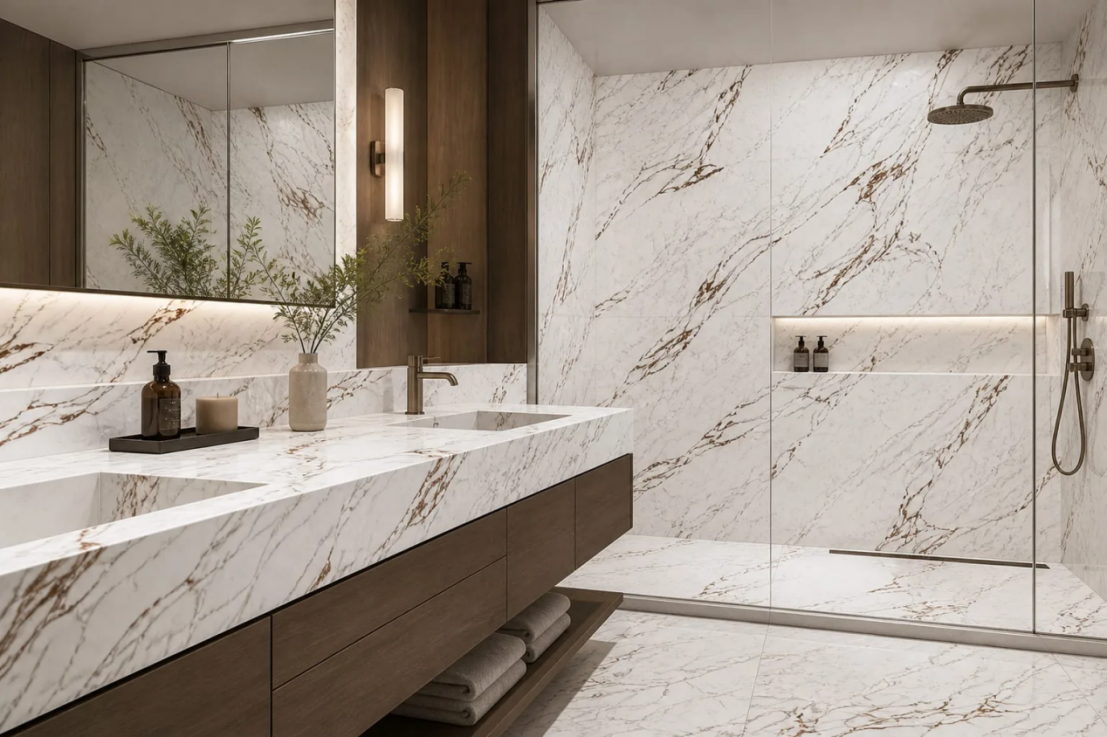
Xiamen, Fujian Sep 29, 2026 (Issuewire.com) - Morning light streams through a bustling residential kitchen in suburban California, casting a warm glow across a seamless artificial quartz island top. Beneath this everyday calm, commercial kitchen countertops and hospitality surfaces endure constant high-frequency use, mechanical impact, and exposure to active liquids.
Choosing the right material for large-scale architectural projects requires more than surface-level aesthetic appeal. Global distributors, contractors, and project developers face strict performance demands when evaluating a Professional Artificial Stone Supplier. Industrial reliability is the foundation of long-term interior success. Evaluating technical data helps stakeholders secure durable results for residential, commercial, hospitality, and architectural developments.
SGS-Tested Industrial Reliability
Reliability in modern engineered stone is defined by verifiable laboratory testing rather than manufacturer claims. SGS-tested industrial reliability refers to rigorous third-party evaluation verifying that artificial quartz slabs meet consistent physical and chemical performance metrics. These benchmarks measure core characteristics such as flexural strength, surface hardness, abrasion resistance, and non-porous liquid containment. For project managers overseeing multi-unit residential or high-traffic hospitality ventures, these tests confirm that the material withstands heavy loads and daily wear without structural degradation.
Technical benchmarks provide objective numerical thresholds for material selection. When assessing artificial quartz slabs, engineers look at water absorption rates, dimensional stability, and thermal resilience. A low water absorption rate prevents moisture penetration, which stops bacterial growth and staining in kitchen environments. By anchoring procurement decisions in certified benchmarks, builders eliminate guesswork and ensure uniform quality across entire shipments of large-format slabs, kitchen islands, and vanity tops.
Common Procurement Pitfalls and Advanced Artificial Quartz Solutions
Procuring architectural stone for international projects involves navigating several recurring risks. Integrating detailed product characteristics, advanced manufacturing craftsmanship, and strict performance metrics helps procurement teams overcome these challenges and secure high-value installations across global markets.
A. Surface Corrosion, Chemical Degradation, and Non-Porous Shielding
Common Challenge: Commercial kitchens and hospitality bars frequently encounter acidic ingredients, cleaning agents, and harsh chemical sanitizers. Selecting unverified stone surfaces often leads to chemical etching, dulling of the polished finish, and permanent staining.
Artificial Quartz Solution: Modern engineered quartz combines refined mineral quartz aggregates with specialized polymer resins under intense vacuum-vibration pressing. This advanced fabrication leaves virtually zero internal micro-voids, producing an exceptionally dense surface structure.
Core Application Value: The non-porous matrix completely blocks liquid penetration, protecting the material against household acids, oils, and chemical sanitizers. Even in high-exposure commercial bar tops and restaurant prep stations, the polished finish resists etching and maintains pristine hygiene standards over years of heavy daily operation.
B. Dimensional Inaccuracy, Edge Warping, and Precision Fabrication
Common Challenge: Precision is critical when installing wall cladding panels, stair components, and custom countertops. Slab thickness variations or warped edges cause alignment gaps during fabrication, leading to costly on-site recutting and project delays.
Artificial Quartz Solution: Cutting-edge production lines utilize computerized calibration and high-tolerance diamond-wire sawing to ensure absolute flatness and uniform thickness across every large-format slab.
Core Application Value: Rigorous quality control checks monitor diagonal dimensions, edge straightness, and thickness consistency. This precise craftsmanship allows fabricators to achieve tight, nearly invisible seams, reducing installation time and eliminating the need for costly on-site adjustments in large commercial projects.
C. Accelerated Lifespan Decay and Mechanical Impact Resistance
Common Challenge: High-traffic public spaces subject flooring, bar tops, and tabletops to constant impact and abrasion. Inferior composite materials develop micro-cracks or surface chipping under heavy structural loads.
Artificial Quartz Solution: Leveraging high percentages of natural quartz crystals bonded with resilient resins, these surfaces achieve superior surface hardness and high flexural strength, absorbing kinetic energy without structural failure.
Core Application Value: The high density and structural cohesion protect against heavy dropped cookware, constant foot traffic, and sharp edge impacts. This mechanical robustness extends the operational lifespan of kitchen islands and commercial counters, reducing replacement cycles in demanding environments.
D. Regulatory Deficits and Compliance Uncertainties
Common Challenge: Importing stone products into North America, Europe, or the Middle East requires compliance with regional safety, hygiene, and material standards. Sourcing from unverified suppliers often results in customs delays or failure to meet local building codes due to missing documentation.
Artificial Quartz Solution: Certified testing protocols and strict quality assurance pathways align every production batch with international food safety and building material regulations.
Core Application Value: Providing complete material traceability and third-party test reports eliminates customs clearance hurdles. Contractors and project developers gain immediate compliance assurance for institutional, hospitality, and residential projects worldwide.
Core Competencies and Technical Innovation at Lexiang Stone
Founded in 2008, Lexiang Import & Export Co., Ltd. operates as a professional supplier and exporter specializing in natural stone and engineered stone products. The company provides comprehensive stone solutions to wholesalers, distributors, contractors, designers, builders, fabricators, and project developers worldwide. The main product range includes natural granite, engineered quartz stone, natural quartzite, large-format slabs, countertop slabs, kitchen countertops, strip slabs, wall cladding panels, bar countertops, kitchen islands, vanity tops, tabletops, and stair components.
Manufacturing innovation centers on optimizing mineral aggregate compaction and resin ratios under high-pressure processing. This technique eliminates internal micro-voids, resulting in a dense, uniform structure. Advanced production lines maintain strict batch consistency for complex projects, ensuring that veining patterns and color tones match seamlessly across large installations. Whether supplying materials for a luxury hotel renovation or a commercial office building, the production framework delivers stable supply and customized processing tailored to exact architectural specifications.
Securing Your Next Project with Proven Stone Solutions
Selecting dependable artificial quartz surfaces transforms architectural concepts into lasting commercial realities. Reviewing physical sample kits and technical datasheets before placing bulk orders ensures complete alignment with project requirements.
For upcoming residential, commercial, or hospitality developments requiring stable supply and certified technical performance, review the complete material range and specifications at the https://www.lxcc.com/
Media Contact
Xiamen Lexiang Import & Export Co., ltd. info@lxcc.com